
Kegelbrecher
Arten von Kegelbrechern Kegelbrecher sind weltweit als “Symons-Typ” bekannt…


Ein Vollflotationsverfahren zur Aufbereitung von polymetallischem Siderit-Erz
1. Technical Field
The present invention relates to a full‑flotation beneficiation method for polymetallic siderite ore, particularly suitable for ores in which siderite is the main mineral, associated with hematite‑limonite, pyrrhotite, pyrite, etc. It belongs to the technical field of mineral processing engineering, specifically iron ore beneficiation.
2. Background Art
Among the proven iron ore reserves, siderite (including pure siderite, hematite, limonite, siderite‑limonite intergrowths, etc.) accounts for less than 10% of the world’s reserves. However, predictions indicate that in the world’s potential iron ore resources, siderite accounts for more than 40%. China is relatively rich in siderite resources, with reserves ranking among the top in the world, totalling about 1.834 billion tonnes. Because siderite has a very fine dissemination size, complex composition, and low grade, iron mainly occurs in the form of carbonates. Part of the siderite forms isomorphous substitution of Fe²⁺ by Mg²⁺ and Mn²⁺, giving magnesium‑manganese siderite, and it is hosted in hematite‑limonite and magnetite. Limonite has a low grade, is complex and difficult to beneficiate, and it is hard to improve both iron grade and recovery; moreover, it tends to slime during grinding, affecting the beneficiation indices. Currently, siderite, limonite and associated complex low‑grade iron ores are recognised as difficult‑to‑process ores. To fully develop low‑grade siderite resources where siderite is the main mineral, conventional physical beneficiation processes such as gravity separation, high‑intensity magnetic separation, flotation, roasting, or combinations thereof have been used abroad. In the 1950s and 1960s, several Eastern European countries built semi‑industrial siderite concentrators, but all suffered from generally low techno‑economic indices. For example, the Bakal concentrator in Ukraine (with a roasting process) could only achieve a concentrate grade of up to 53%; the Dnani concentrator in Czechoslovakia, using a magnetic‑flotation combined flowsheet, obtained an iron concentrate grade of only about 35%. In Germany, the Siegerland plant treating manganese‑bearing siderite produced an iron concentrate grade of 50% with a recovery of 62.8%. To date, there is no industrial practice solely for siderite beneficiation either domestically or internationally. Daye Iron Mine and Jiuquan Iron Mine can recover a portion of associated siderite in their iron ore processing flowsheets, but only obtain a siderite concentrate containing about 35% Fe.
Siderite is a carbonate‑type mineral; its iron grade increases considerably after roasting. Although roasting can yield a higher‑grade iron concentrate, the double‑roasting cost is very high. If the iron grade is upgraded to about 39% by conventional physical beneficiation, and then the product is pelletised and sintered, the iron grade can be raised to about 55%, thus saving one roasting step and improving economic returns. Likewise, high‑intensity magnetic separation consumes large amounts of electricity and water, has high costs, and is difficult to commercialise.
Currently, there is no successful practical experience with full‑flotation for siderite, mainly due to the difficulty in selecting a suitable collector for siderite, and also because the harmful elements sulfur and phosphorus are relatively high and tend to be incorporated into the siderite concentrate during flotation, making it difficult to obtain a siderite concentrate that meets smelting requirements. Therefore, applying full‑flotation to siderite beneficiation is of great significance.
3. Summary of the Invention
The objective of the present invention is to provide a full‑flotation beneficiation method for polymetallic siderite ore. For siderite ores with high sulfur content and associated valuable element copper, as well as minor amounts of hematite‑limonite, pyrrhotite and pyrite, the full‑flotation flowsheet can yield a siderite concentrate with Fe grade ≥38%, iron recovery 75‑80%, and sulfur content <0.20%; a copper concentrate with Cu grade ≥18% and recovery ≥70%; and a sulfur concentrate with S grade ≥45% and recovery ≥70%. In the present invention, a special siderite collector is used, which enables strong physicochemical adsorption between the siderite surface and the collector, thereby achieving effective separation of siderite from other non‑target minerals.
The method comprises the following steps:
(1) Crush the raw siderite ore to below ‑3 mm and homogenise. Then feed into a ball mill at a liquid‑to‑solid weight ratio of 1:2, grinding to a pulp where the particle size of ‑0.074 mm accounts for 75‑95% and ‑0.100 mm accounts for 100% or more.
(2) Copper‑sulphur bulk flotation:
(3) Copper‑sulphur separation flotation:
Add activated carbon for de‑reagent at 200‑400 g/t ore, stir 5‑10 min. Add lime at 3000‑6000 g/t ore to adjust pH to 12‑14, stir 3‑6 min. Add 2# oil at 20‑40 g/t ore, stir 2‑4 min; aerate and scrape froth for 2‑4 min.
(4) Copper cleaner stages:
(5) Sulphur cleaner stages:
(6) Siderite roughing stage:
Add activated carbon for de‑reagent at 200‑400 g/t ore, stir 5‑10 min. Use sodium hexametaphosphate as a regulator to improve pulp dispersion, at 400‑800 g/t ore, stir 3‑6 min. Adjust pH to 5‑6 with sulfuric acid, stir 3‑6 min. Add starch as depressant at 500‑800 g/t ore, stir 3‑6 min. Add SP‑type collector at 400‑800 g/t ore, stir 3‑6 min. Add 2# oil as frother at 10‑40 g/t ore, stir 3‑6 min. Aerate and scrape froth; the froth product goes to the next stage of reverse flotation for sulfur and phosphorus reduction.
(7) Siderite cleaner stages:
The said SP‑type collector has been disclosed in patent application No. 200810058134.3, and its formulation and preparation are as follows:
Raw materials: dodecylamine (S₁), mixed amine (S₂), ether amine (S₃), naphthenic acid {CHzn‑COOH} (S₄), sulfuric acid (P₁), hydrochloric acid (P₂), caustic soda (P₃).
Weight ratio:
S = dodecylamine S₁ : mixed amine S₂ : hydrochloric acid P₂ = 20‑40 : 20‑40 : 80‑20
P = ether amine S₃ : naphthenic acid S₄ : caustic soda P₃ : sulfuric acid P₁ = 10‑30 : 20‑50 : 10‑20 : 60‑10
SP = S : P = 10‑80 : 90‑20.
Purity specifications: dodecylamine ≥96%, mixed amine ≥95%, hydrochloric acid (concentration by weight) ≥35%; sulfuric acid (concentration by weight) ≥95%, caustic soda ≥96%, ether amine ≥98%, naphthenic acid ≥98%.
Preparation method for the SP collector:
Advantages and positive effects compared with known technologies:
By adopting the full‑flotation flowsheet for polymetallic siderite ores, a siderite concentrate with Fe grade >39%, recovery 75‑80%, and sulfur content <0.15% is obtained; a copper concentrate with Cu grade >18% and recovery >71%; and a sulfur concentrate with S grade >39%, recovery >75%, and sulfur content <0.15%. The method achieves effective separation of siderite from other minerals, providing an effective beneficiation process for utilising China’s relatively abundant siderite resources.
4. Brief Description of Drawings
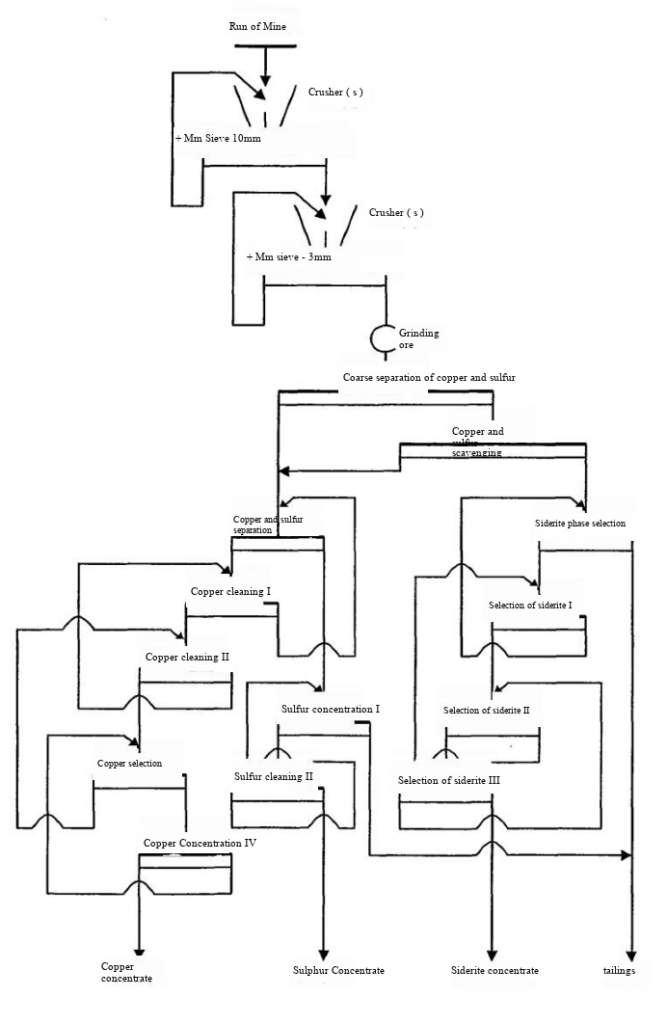
Figure 1 is the full‑flotation flowsheet of the present invention for siderite ore.
5. Detailed Description of Embodiments
Beispiel 1:
The raw material comes from the Shangchang Wangjiatan siderite mine of Kunming Iron & Steel Group Co., Ltd., with associated valuable copper that needs comprehensive recovery. Mineralogical analysis shows this siderite is a typical magnesium‑manganese siderite. Run‑of‑mine ore contains TFe 27‑29%. The sulfur‑bearing mineral analysis is shown in Table 1, and the chemical composition of the raw ore in Table 2. Using the full‑flotation flowsheet of Figure 1, the ore is crushed to below ‑3 mm, homogenised, and ground in a ball mill at a liquid‑to‑solid weight ratio of 1:2 to a grinding fineness of 90% passing 0.074 mm.
Copper‑sulphur bulk flotation:
Copper‑sulphur separation: activated carbon 300 g/t ore, stir 5‑10 min; lime 4000 g/t ore to adjust pH to 12‑14, stir 3‑6 min; 2# oil 30 g/t ore, stir 2‑4 min; aerate and scrape 2‑4 min.
Copper cleaners:
Sulphur cleaners:
Siderite roughing: activated carbon 200 g/t ore, stir 5‑10 min; sodium hexametaphosphate as dispersant 500 g/t ore, stir 3‑6 min; adjust pH to 5‑6 with sulfuric acid, stir 3‑6 min; starch as depressant 600 g/t ore, stir 3‑6 min; SP collector 800 g/t ore, stir 3‑6 min; 2# oil 30 g/t ore, stir 3‑6 min; aerate and scrape froth, sending the froth product to the next reverse flotation for sulphur and phosphorus removal.
Siderite cleaners:
The recoveries obtained are: Fe in siderite concentrate 75.98%, Cu in copper concentrate 72.59%, S in sulphur concentrate 82.85%.
Equipment used: ball mill Φ900×1800 mm, jaw crusher Φ10×50 mm and Φ3×30 mm, self‑aeration flotation cells (single cell volume 3 m³) manufactured by kenex Mining Machinery Factory, spiral classifier Φ2000 mm, hydrocyclone Φ150 mm.
Table 1 Analysis of raw mineral content
| mineral | Siderite | goethite | magnetite | Ferric silicate | Gangue and others |
| content(%) | 50.46 | 4.57 | 0.27 | 6.57 | 38.13 |
Table 2 Chemical composition analysis of raw ore
| Projekt | Fe | S | P | Da | Cu | Mn | MgO | SiO₂ |
| content(%) | 29.98 | 1.87 | 0.048 | 0.008 | 0.22 | 6.16 | 10.54 | 22.12 |
Tabelle 3 Process mineral processing indicators
| productname | Yield(%) | grade(%) | Recovery rate (%) | ||||
| Fe | S | Cu | Fe | S | Cu | ||
| copper concentrate | 0.88 | 22.46 | 13.26 | 18.15 | 0.66 | 6.20 | 72.59 |
| Sulfur concentrate | 3.16 | 34.17 | 48.94 | 0.93 | 3.60 | 82.25 | 13.36 |
| Siderite Concentrate | 56.70 | 40.19 | 0.132 | 0.031 | 75.98 | 3.98 | 7.99 |
| Tailings | 39.26 | 15.09 | 0.362 | 0.034 | 19.76 | 7.57 | 6.06 |
| Mineral feed | 100.00 | 29.99 | 1.88 | 0.22 | 100.00 | 100.00 | 100.00 |
Example 2:
The raw material comes from a siderite mine in Shaanxi Province, China, with associated valuable copper that requires comprehensive recovery and utilization. Mineralogical analysis shows that this siderite is a typical magnesium-manganese siderite. The run-of-mine ore contains about 30% TFe. The sulfur-bearing mineral content analysis is shown in Table 4, and the chemical composition of the raw ore is shown in Table 5. Using the full-flotation flowsheet of Figure 1,
the grinding fineness is 85% passing 0.074 mm, and 100% passing 0.100 mm.
The flotation reagent regime is as follows:
The recoveries obtained are: Fe in siderite concentrate 76.40%, Cu in copper concentrate 71.99%, and S in sulfur concentrate 80.20%.
Table 4 Analysis of raw mineral content
| mineral | Siderite | goethite | magnetite | Ferric silicate | Gangue and others |
| content(%) | 49.82 | 3.48 | 0.42 | 4.57 | 41.71 |
Table 5 Chemical composition analysis of raw ore
| Projekt | Fe | S | P | Da | Cu | Mn | MgO | SiO₂ |
| content(%) | 28.76 | 1.82 | 0.039 | 0.007 | 0.21 | 4.28 | 9.94 | 21.69 |
Tabelle 6 Process mineral processing indicators
| productname | Yield(%) | grade(%) | Recovery rate (%) | ||||
| Fe | S | Cu | Fe | S | Cu | ||
| copper concentrate | 0.83 | 21.52 | 14.96 | 18.23 | 0.62 | 6.79 | 71.99 |
| Sulfur concentrate | 2.98 | 33.69 | 49.25 | 0.86 | 3.49 | 80.20 | 12.19 |
| Siderite Concentrate | 55.12 | 39.86 | 0.128 | 0.032 | 76.40 | 3.85 | 8.39 |
| Tailings | 41.07 | 13.65 | 0.408 | 0.038 | 19.49 | 9.16 | 7.43 |
| Mineral feed | 100.00 | 28.76 | 1.83 | 0.21 | 100.00 | 100.00 | 100.00 |
| Fe | S | .Cu | Fe | S | Cu | ||
| copper concentrate | 3.46 | 21.18 | 11.92 | 25.80 | 2.29 | 20.32 | 87.53 |
| Sulfur concentrate | 3.11 | 31.22 | 48.98 | 0.68 | 3.03 | 75.04 | 2.07 |
| Siderite Concentrate | 60.73 | 42.19 | 0.06 | 0.11 | 79.99 | 1.79 | 6.55 |
| Tailings | 32.70 | 14.39 | 0.177 | 0.12 | 14.69 | 2.85 | 3.85 |
| Mineral feed | 100.00 | 32.03 | 2.03 | 1.02 | 100.00 | 100.00 | 100.00 |





 English English
 Spanish
 Russian
 Arabic
 Swahili
 French
 Turkish
 Portuguese
 Korean
 Japanese
 German
 Italian